

Engineer's Toolbox
Visit www.hansarobotics.com

A Filter Materials Lamination Machine bonds filter layers into a stable, functional composite. It may combine nonwoven fabric, melt-blown media, wire mesh, film, or support paper. The machine controls pressure, heat, adhesive application, and web tension. These variables shape filtration performance and production consistency.
In practical manufacturing, operators watch the material as it passes between heated rollers. A slight wrinkle can affect sealing, airflow, or pleat formation. Reliable machines often include tension controls, temperature sensors, alignment systems, and adjustable lamination speeds. However, automation does not remove every risk. Incorrect settings may damage delicate fibers or create uneven bonding. This is where process knowledge matters.
Good equipment selection begins with the filter design. Engineers should review material thickness, thermal sensitivity, adhesive compatibility, line speed, and required bond strength. Testing should include peel strength, air permeability, dimensional stability, and visual inspection. Supplier data is useful, but it should not replace production trials. Real materials behave differently.
Small details matter.
A clear operating record can reveal problems early. It can also support repeatable quality checks across different batches. This guide explains how a Filter Materials Lamination Machine works, where it fits in filter production, and which specifications deserve careful attention. Some applications may need customized rollers, cleaning systems, or curing stages. The best solution is not always the fastest one. Reliability, maintainability, and verified performance should guide the final decision.
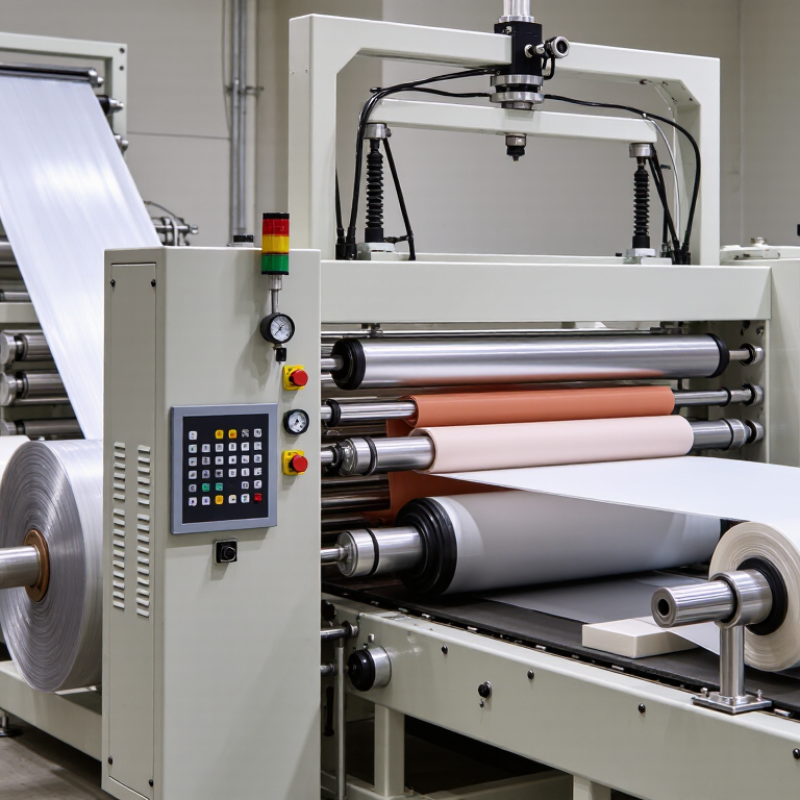
A filter materials lamination machine is industrial equipment designed to bond multiple filter layers into one functional structure. It joins media, support fabrics, meshes, or protective films with controlled heat, pressure, or adhesive. The core purpose is to create a stable composite without damaging the filter’s pores. This structure can improve handling, durability, and resistance to separation during installation or use.
In a typical line, separate rolls unwind at a controlled speed. Tension systems keep each layer flat and aligned. Heated rollers, pressure rollers, or adhesive coating units then combine the materials. Operators monitor temperature, line speed, nip pressure, and adhesive coverage. Small adjustments can change the final result. This is where experience matters.
A reliable lamination process must protect airflow, filtration efficiency, and mechanical strength. The bonded material should not wrinkle, peel, or seal important pores. Technicians usually inspect samples and test peel strength, thickness, and visual uniformity. Practical trials often reveal problems that specifications miss. The process is not flawless. An apparently smooth surface can still hide weak bonding. Humidity, coating weight, and roll alignment may shift performance. For this reason, careful records and measured adjustments remain essential when setting up production.
| Dimension | Definition or Function | Typical Technical Information | Practical Importance |
|---|---|---|---|
| Equipment Definition | A filter materials lamination machine is industrial equipment that bonds two or more layers of filter media, support materials, films, meshes, or nonwoven fabrics into a composite structure. | The machine may use heat, pressure-sensitive adhesive, hot-melt adhesive, ultrasonic energy, or other controlled bonding methods. | It creates a multilayer filter material with more stable handling, improved strength, and controlled functional performance. |
| Core Purpose | The primary purpose is to join separate material layers continuously and uniformly while preserving the required filtration, airflow, and structural properties. | Key controls generally include web tension, bonding pressure, temperature, line speed, adhesive application, and material alignment. | Consistent lamination helps reduce delamination, wrinkles, weak bonds, and variations in finished filter quality. |
| Common Input Materials | Input materials can include melt-blown media, spunbond nonwovens, needle-punched fabrics, filtration paper, synthetic membranes, woven meshes, and protective films. | Materials are commonly supplied in rolls and may differ in thickness, porosity, basis weight, surface energy, and heat sensitivity. | Material compatibility determines the suitable bonding method and operating window. |
| Typical Product Structures | Laminated products may contain a filtration layer combined with a support layer, pre-filter layer, scrim, membrane, drainage layer, or protective facing. | Examples include two-layer, three-layer, and multilayer constructions used in air, liquid, medical, industrial, and automotive filtration. | Layer selection allows a product to combine filtration efficiency, mechanical support, protection, and processability. |
| Bonding Methods | Bonding can be achieved through thermal calendering, hot-melt adhesive coating, powder or web adhesive, flame lamination, ultrasonic bonding, or pressure-sensitive adhesive systems. | Thermal methods require controlled heat and nip pressure; adhesive methods additionally require coating-weight and curing or cooling control. | The method affects bond strength, flexibility, air permeability, chemical resistance, and the risk of blocking or media damage. |
| Feeding and Web Handling | Roll-to-roll feeding systems guide, unwind, align, and combine continuous material webs before bonding. | Typical features include unwind stands, tension controllers, edge guides, splice handling, web guides, and synchronized drive systems. | Stable web handling helps maintain layer registration and prevents stretching or creasing of delicate filter media. |
| Temperature Control | Temperature control is used when the bonding process depends on heat activation, melting, softening, or drying. | Heated rollers, hot-air zones, infrared heaters, or heated platens may be used, depending on the process design. | Accurate temperature control supports repeatable bonding while limiting thermal shrinkage, melting, odor, or deformation. |
| Pressure and Nip Control | Nip pressure brings the layers into contact and helps distribute heat or adhesive across the bonding area. | Pressure may be adjusted mechanically, hydraulically, or pneumatically; the correct setting depends on material thickness and compressibility. | Proper pressure improves bond uniformity without excessively compressing pores or reducing airflow. |
| Line Speed | Line speed is the rate at which the material web passes through the lamination zone. | Speed is normally expressed in metres per minute and must be balanced with heating, adhesive setting time, pressure, and web tension. | Higher speed can increase output, but inadequate process energy or residence time may reduce bonding quality. |
| Adhesive Application | When adhesive lamination is used, the machine applies a controlled amount of adhesive between selected layers. | Application formats may include dots, lines, spray patterns, grids, films, powders, or full-surface coatings. | A controlled pattern preserves flexibility and air permeability while providing sufficient bond coverage. |
| Quality Control Parameters | Quality checks evaluate whether the laminated material meets required structural and filtration-related specifications. | Common checks include peel or bond strength, thickness, basis weight, width, appearance, air permeability, pressure drop, and layer alignment. | Monitoring these parameters helps identify process drift and supports stable downstream converting and assembly. |
| Filtration Performance Considerations | The lamination process must maintain the functional properties of the filter media rather than obstructing or damaging the active filtration layer. | Important factors include pore structure, air or liquid permeability, pressure drop, filtration efficiency, and resistance to the intended operating environment. | Excessive adhesive, heat, or compression can reduce permeability or alter the designed filtration performance. |
| Automation and Monitoring | Modern systems may use sensors and control units to regulate tension, temperature, pressure, speed, adhesive delivery, and web position. | Monitoring may include digital recipe control, alarm systems, closed-loop tension control, and production data recording. | Automation improves repeatability, reduces operator-dependent variation, and supports faster changeovers. |
| Typical Applications | Laminated filter materials are used in air filtration, liquid filtration, dust collection, respiratory protection, cleanroom products, automotive systems, and industrial process filtration. | The final material may be converted into cartridges, panels, bags, masks, pleated elements, or other filter assemblies. | Different applications require different combinations of filtration efficiency, strength, chemical resistance, and permeability. |
| Main Benefits | Lamination can improve dimensional stability, tear resistance, handling strength, layer protection, and product integration. | Benefits depend on the selected materials and bonding process; lamination does not automatically improve every filtration characteristic. | The process enables engineered multilayer media designed for specific performance and manufacturing requirements. |
| Operational Safety | Operators must manage moving webs, heated surfaces, nip points, adhesive systems, and electrical or pneumatic components. | Important safeguards include guarding, emergency stops, temperature protection, ventilation where required, and lockout procedures for maintenance. | Proper safety controls reduce the risk of burns, entanglement, exposure, and equipment-related injuries. |